Selecting the right type of welding determines your production speed, weld integrity, and overall shop efficiency. Fabricators often choose between the targeted stud welding process and traditional Metal Inert Gas (MIG) joining. While both create strong metal bonds, their execution differs significantly.
The technical breakdown below compares cycle speeds, structural performance, and equipment demands for modern manufacturing environments.
| Performance Metric | Stud Welding Process | MIG Welding |
| Average Cycle Time | 0.005 – 1.5 seconds | 30 – 120+ seconds |
| Heat-Affected Zone (HAZ) | Minimal to localized | Moderate to widespread |
| Single-Sided Access | Yes (100%) | Requires clear access |
| Reverse-Side Marking | None (CD) / Low (Arc) | High risk of distortion |
Understanding the Stud Welding Process in Modern Production
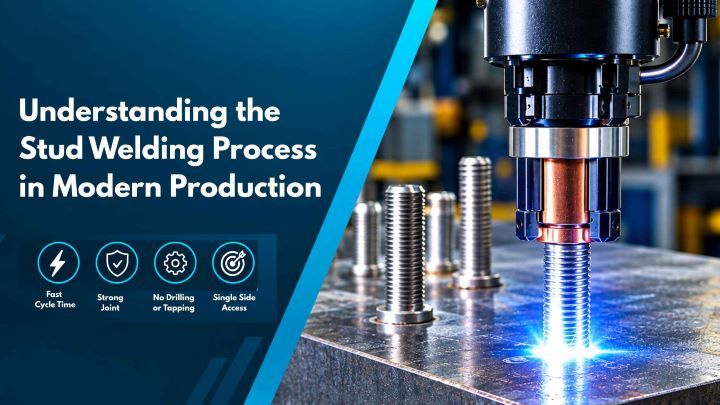
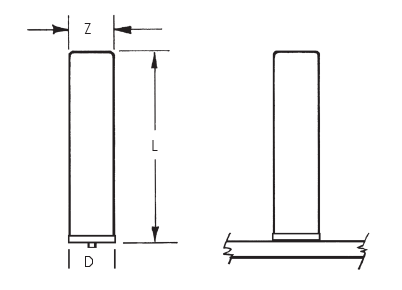
The stud welding process joins a metal fastener to a base metal workpiece instantaneously using an electric arc. Unlike conventional fillet welding, this method joins the full cross-sectional area of the fastener without drill holes, tapping, or secondary grinding. Therefore, it delivers full-penetration joint strength in a fraction of a second.
The Arc Stud Welding Process
For heavy-duty structural applications, the ARC stud welding process utilizes a DC power source to draw an arc between the fastener end and the base metal. As a result, it creates a molten pool while a ceramic ferrule shields the arc and contains the molten metal.
According to AWS D1.1 structural welding standards, drawn arc cycles last between 0.1 and 1.5 seconds, delivering tensile strength that reliably exceeds the yield point of the fastener itself.
The Capacitor Discharge Stud Welding Process
For thin sheet metals, the Capacitor Discharge stud welding process relies on a bank of storage capacitors. The system releases stored electrostatic energy in 1 to 6 milliseconds. Consequently, this ultra-fast discharge prevents heat burn-through and distortion on back-side painted or galvanized surfaces.
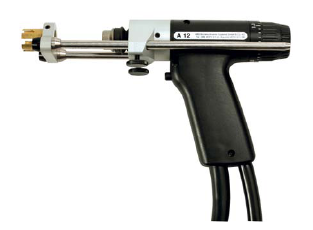
Manufacturers integrate heavy-duty stud welding systems and precise stud welding equipment into automated lines to boost daily output. Specialized stud welding machines from Complete Stud Welding ensure consistent melt depth and repeatable quality across thousands of cycles.
Technical Comparison: MIG Welding Equipment vs Stud Systems
Traditional MIG joining requires a continuously fed solid wire electrode (such as AWS ER70S-6 with 70,000 PSI tensile strength) and an external shielding gas. While a standard MIG welder or MIG welding machine works exceptionally well for long seam welds, attaching point fasteners with MIG welder equipment introduces severe operational bottlenecks.
The following technical comparison highlights the key differences between standard MIG welding equipment and dedicated stud systems:
| Technical Parameter | Stud Welding Systems | MIG Welding Equipment |
| Cycle Speed | 0.005 to 1.5 seconds per stud | 30 to 120 seconds per stud |
| Heat-Affected Zone (HAZ) | Extremely localized; minimal heat input | Widespread continuous thermal input |
| Cross-Sectional Fusion | 100% full cross-sectional weld area | Periphery fillet weld bead only |
| Reverse-Side Marking | Zero marking (CD) / Low heat distortion (Arc) | High risk of burn-through and distortion |
| Substrate Hole Preparation | None required | Requires drilling or tapping for through-fasteners |
| Workpiece Access | Single-sided access required | Requires clear surrounding torch access |
Key Advantages for Industrial Fastening Solutions
When evaluating an industrial fastening solution, production engineers must weigh cycle times, structural specifications, and overall assembly costs.
Speed and Production Throughput
Because a stud weld takes less than two seconds, shops can achieve high production speeds. Transitioning from manual arc feeds to automatic stud units reduces labor costs and prevents production bottlenecks.
Structural Reliability
Because the weld zone covers the full diameter of the fastener, the connection resists extreme vibrational, shear, and tensile forces. As a result, the fastener will typically bend or break within its own shank before the weld interface fails.
Single-Sided Access
Stud fasteners require access to only one side of the workpiece. This eliminates drilling, tapping, hole-punch alignment, and reverse-side leak paths in fluid containers.
Selecting the Right Equipment for Your Operational Needs
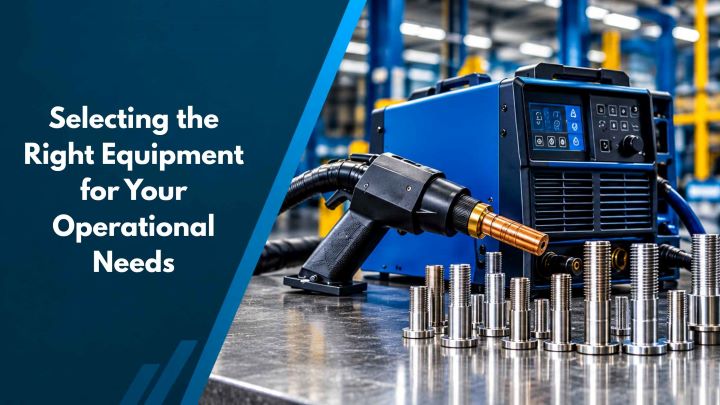
Choosing between these processes depends on your application geometry and fastener design:
- Use a MIG setup when welding structural beams, filling wide gaps, or running long continuous seam joins on heavy fabrications.
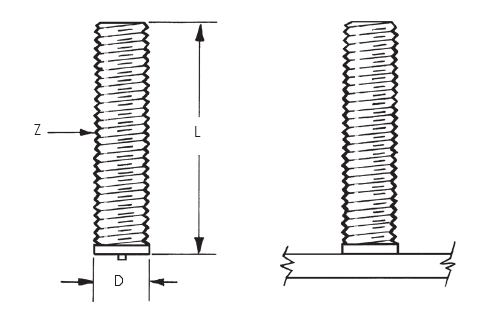
- Use Stud Welding when attaching threaded pins, shear connectors, or insulation fasteners to flat or curved metal surfaces efficiently.
For specialized applications, using the right machine makes all the difference. Check out our guide on ARC Weld Studs Applications in Modern Manufacturing to see real-world industry implementations. You can also explore our technical overview on the Ceramic Ferrule for Arc Stud Welding to learn how arc shielding optimizes weld quality.
Optimize Your Production Line with Complete Stud Welding
Since 1988, Complete Stud Welding has delivered industry-leading fastener solutions, equipment sales, and rental fleets across North America. Whether you need portable capacitor discharge units, heavy-duty arc power sources, or custom weld studs, our technical team helps you select the exact setup for your shop floor.
Visit our Stud Welding Equipment directory to review machine specifications and rental options. Call our application engineers today at 216-904-4008 for technical support, equipment quotes, and joint evaluation.


Comments are closed.